Steam Boiler Fuel Cost: Gas vs Biomass vs Electric
Contents Hide 1 Introduction 2 1. What Determines Steam Boiler Fuel Cost? 2.1 1.1 Delivered Energy Tariffs 2.2 1.2 Thermal Conversion Efficiency 2.3 1.3 Operating Steam Pressure 2.4 1.4 Feedwater Temperature 2.5 1.5 Condensate Recovery Rate 3 2. How to Calculate Steam Boiler Fuel Consumption 4 3. Gas Steam Boiler Fuel Cost 4.1 3.1 Natural […]
Get Instant Quote
Technical Specifications
Introduction
How much does it cost to produce one ton of industrial steam?
Plant engineers and procurement directors frequently evaluate competing fuel options before purchasing equipment. However, comparing unit Steam Boiler Fuel Cost alone produces misleading operating budget estimates.
A comprehensive financial evaluation requires a balance of several core engineering factors:
Natural gas, solid biomass, and electric power each present distinct thermodynamic properties, capital cost profiles, and operating cost curves. This selection guide provides engineering calculation models, operational benchmarks, and cost comparisons to help you select the most economical fuel source for your plant.
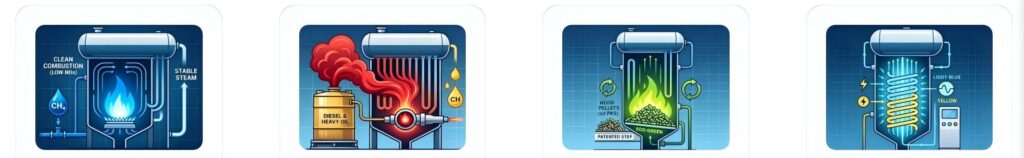
1. What Determines Steam Boiler Fuel Cost?
Steam Boiler Fuel Cost depend on five fundamental thermodynamic and site-specific parameters:
1.1 Delivered Energy Tariffs
Fuel tariffs vary substantially across global markets. Pipeline natural gas rates depend on local utility infrastructure and regional extraction access. Solid biomass pricing fluctuates based on agricultural seasons, processing quality, and trucking radius. Industrial electricity rates reflect grid capacity, peak demand surcharges, and transformer configurations.
1.2 Thermal Conversion Efficiency
Boiler design determines how effectively a system transfers fuel combustion energy into saturated steam. Modern gas-fired boilers with condensing economizers reach 95% to 98% thermal efficiency. Solid biomass boilers operate between 80% and 86% efficiency due to flue gas moisture and solid-fuel combustion characteristics. Electric steam generators deliver 98% to 99% conversion efficiency at the heating elements.
1.3 Operating Steam Pressure
Generating steam at higher pressures requires more heat input per kilogram of water. A system operating at 1.6 MPa requires more fuel per ton of output than a low-pressure 0.7 MPa system. The target process pressure directly dictates the required enthalpy input:
- 0.7 MPa (7 bar / 100 psi): Lower heat input, thinner vessel walls
- 1.0 MPa (10 bar / 145 psi): Standard industrial heating process baseline
- 1.25 MPa (12.5 bar / 180 psi): Common textile, dyeing, and chemical reactor pressure
- 1.6 MPa to 2.5 MPa+: Demanding refinery, autoclave, and power generation duties
1.4 Feedwater Temperature
Raising cold makeup water from 15°C to boiling demands significantly more fuel energy than heating pre-treated feedwater at 85°C. Every 6°C increase in boiler feedwater temperature reduces fuel consumption by approximately 1%.
1.5 Condensate Recovery Rate
Returning hot condensate back to the deaerator saves both water and thermal energy. High condensate return rates reduce the amount of cold makeup water entering the system, lowering boiler fuel consumption and water treatment costs.
2. How to Calculate Steam Boiler Fuel Consumption
To establish a baseline for your plant, use thermodynamic first principles to model fuel consumption per ton of steam.
3. Gas Steam Boiler Fuel Cost
Natural gas serves as the global industrial benchmark for automatic, high-efficiency steam generation.
3.1 Natural Gas Consumption Factors
Operating a standard gas-fired industrial steam boiler typically requires between 68 and 74 Nm³ of natural gas to produce one ton of saturated steam at 1.0 MPa (assuming 20°C ambient makeup water and 92% efficiency).
Integrating a condensing flue gas heat recovery unit drops consumption to 64 to 68 Nm³/ton.
3.2 Operational Advantages of Natural Gas
- Automated Modulation: Electronic air-fuel ratio controls match dynamic factory steam demand within seconds.
- Compact Boiler Footprints: Eliminates on-site fuel yards, transfer conveyors, and ash silos.
- Low Emissions: Minimal sulfur dioxide (SO 2) and particulate emissions; low-NOx burners meet strict regional limits.
- Low Auxiliary Power Usage: Smaller forced-draft fans draw significantly less electricity than biomass draft fans.
3.3 Hidden Costs in Gas Fired Systems
- Pipeline connection charges, civil metering stations, and pipeline pressure booster compressors.
- Dedicated gas pressure regulating trains and gas leak detection networks.
- Exposure to regional gas market rate adjustments.
4. Biomass Steam Boiler Fuel Cost
Solid biomass boilers provide an economical alternative where local timber, agricultural processing, or crop waste can be sourced at low transport costs.
4.1 Specific Fuel Consumption by Biomass Type
Due to varying moisture levels and lower calorific values, solid biomass consumption rates run higher than gas by total mass:
- High-grade Wood Pellets: 150 to 180 kg per ton of steam
- Dry Wood Waste / Sawdust (15% moisture): 180 to 220 kg per ton of steam
- Wet Wood Chips (40% moisture): 260 to 340 kg per ton of steam
- Rice Husks: 210 to 260 kg per ton of steam
4.2 Biomass Cost Variables
Do not assess solid biomass solely by the purchase price per metric ton. Sourcing evaluations must factor in:
- Moisture Content (Mw): Higher moisture content diverts combustion heat to evaporate internal water, lowering boiler efficiency.
- Ash Content & Slagging Potential: High-silica fuels (e.g., rice husk) require continuous ash discharge and frequent maintenance.
- Transportation Radius: Bulk biomass has low energy density. Long trucking distances can double effective fuel costs.
- Storage and Handling Losses: Uncovered fuel yards risk rain soaking, decomposition, and spontaneous combustion hazards.
5. Electric Steam Boiler Operating Cost
Electric steam generators utilize direct-immersion heating elements or electrode assemblies to heat boiler water.
5.1 Operating Cost Equation
The electric steam boiler operating cost relies on one primary operational metric:
Producing one ton of steam from 20°C feedwater requires 690 to 720 kWh of electric power. At an industrial tariff of $0.10/kWh, the fuel cost alone reaches $69.00 to $72.00 per ton of steam, which is significantly higher than equivalent natural gas or biomass systems.
5.2 Advantages
- Minimal Infrastructure: Eliminates fuel storage, supply piping, chimneys, and burners.
- Zero On-Site Emissions: No exhaust flue, low noise levels, and zero combustion permits required.
- Small Physical Footprint: Can be installed close to steam-consuming machines, reducing distribution heat losses.
5.3 Technical Constraints
- Requires substantial transformer and switchgear capacity. A 2 TPH electric boiler demands roughly 1.5 MW of continuous dedicated power.
- High peak-hour demand charges and power capacity fees.
6. Gas vs Biomass vs Electric: Technical Comparison
| Engineering Parameter | Natural Gas Fired | Solid Biomass Fired | Electric Immersion / Electrode |
|---|---|---|---|
| Typical Thermal Efficiency | 92% – 98% (with Economizer) | 80% – 86% | 98% – 99% |
| Fuel Energy Density | High (~35.8 MJ/Nm³) | Low to Medium (10.5–18.0 MJ/kg) | Direct Power Transfer |
| Combustion Footprint | Compact | Large (Includes fuel yard & silo) | Extremely Compact |
| Fuel Handling Complexity | Low (Direct Pipeline) | High (Conveyors, hoppers, stokers) | None |
| Auxiliary Power Consumption | Low (15–30 kWh/ton steam) | High (45–80 kWh/ton steam) | Baseline Only |
| Flue Gas Filtration Needs | None (Clean combustion) | Multi-cyclone / Baghouse filter | None |
| Combustion Automation | Fully automated PLC control | Semi- to fully automated | Instantaneous electronic control |
| Equipment CAPEX Profile | Moderate | High (2.0× to 3.0× Gas) | Low |
| Typical OPEX Profile | Moderate (Tied to pipeline gas) | Lowest (With local biomass waste) | Highest (Tied to power tariffs) |
| Optimal Production Duty | Continuous industrial processing | High-capacity continuous baseload | Intermittent, clean, or micro plants |
7. Cost per Ton of Steam: Calculation Framework
To calculate the cost per ton of steam for your plant, use this step-by-step framework:
8. Annual Operating Cost Case Study (5 TPH System)
The following financial model compares fuel costs for a production plant operating a 5 TPH steam boiler for 6,000 hours annually (producing 30,000 tons of steam per year at 1.0 MPa, with 20°C makeup water).
Cost Comparison Table
| Metric / Parameter | Natural Gas Boiler (94% Efficiency) | Wood Pellet Boiler (84% Efficiency) | Industrial Electric Boiler (99% Efficiency) |
|---|---|---|---|
| Energy Consumption per Ton | 70 Nm³ / Ton | 175 kg / Ton | 705 kWh / Ton |
| Assumed Local Energy Price | $0.45 / Nm³ | $110 / Metric Ton | $0.09 / kWh |
| Direct Fuel Cost per Ton | $31.50 / Ton | $19.25 / Ton | $63.45 / Ton |
| Auxiliary Electrical Cost | $1.80 / Ton | $4.50 / Ton | $0.20 / Ton |
| Water, Chemicals & Labor | $2.20 / Ton | $4.80 / Ton | $1.10 / Ton |
| Total Operating Cost per Ton | $35.50 / Ton | $28.55 / Ton | $64.75 / Ton |
| Total Annual Fuel OPEX | $945,000 / year | $577,500 / year | $1,903,500 / year |
| Total Annual Operating Cost | $1,065,000 / year | $856,500 / year | $1,942,500 / year |
Note: The figures above reflect standard baseline project modeling. Enter your local energy tariffs to calculate project-specific returns.
In this operating scenario, the biomass boiler saves $208,500 per year over the natural gas system. However, it requires a larger initial capital investment for fuel storage and automated conveying systems.
To review equipment pricing and compare initial investments, see our comprehensive guide on industrial steam boiler price and complete TCO.
9. Fuel Cost vs. Total Steam Production Cost
Direct fuel expenses make up the largest share of operating costs, but calculating your overall cost per ton of steam requires accounting for all auxiliary operations:
- Auxiliary Power: Heavy draft fans, high-pressure feedwater pumps, fuel conveyors, and electrostatic precipitators consume electricity.
- Water Softening & Chemicals: Removing mineral hardness and dosing scale inhibitors, oxygen scavengers, and neutralizing amines.
- Maintenance & Refractory: Routine servicing for grate bars, burner nozzles, gaskets, safety relief valves, and firebrick refractory lining.
- Solid Residue Handling: Biomass combustion requires dedicated ash collection, handling, and disposal.
10. How Efficiency Impacts Steam Boiler Fuel Cost
Higher thermal efficiency directly lowers your annual fuel bills.
Consider a 10 TPH Natural Gas Boiler operating for 6,000 hours per year at an average tariff of $0.45/Nm³:
- Boiler A (89% Efficiency – Basic Design): Consumes 73.9 Nm3/ton. Annual fuel cost: $1,995,300.
- Boiler B (95% Efficiency – Condensing Economizer): Consumes 69.2Nm3/ton. Annual fuel cost: $1,868,400.
- Net Annual Savings: $126,900 every year.
A high-efficiency boiler with an economizer costs roughly $35,000 to $50,000 more upfront. The fuel savings completely recover that price difference within 4 to 6 months of continuous operation.
11. How Condensate Recovery Reduces Fuel Expenses
Discharging condensate is one of the most common causes of wasted fuel in industrial steam systems.
Returning hot condensate (80°C to 95°C) to the feedwater tank lowers fuel costs in four distinct ways:
- Saves Fuel: Less fuel is needed to heat hot condensate back into steam compared to cold makeup water.
- Cuts Water Costs: Reusing condensed water reduces utility water bills.
- Lowers Chemical Use: Condensate is distilled water, meaning fewer softening and conditioning chemicals are required.
- Reduces Blowdown Heat Losses: Pure return water keeps total dissolved solids (TDS) low, reducing the need for boiler blowdown.
Recovering 60% of plant condensate typically lowers net fuel consumption by 6% to 10%. For detailed plant engineering, see our complete guide on industrial boiler selection and capacity planning.
12. Fuel Selection Guide: Matching Fuel to Factory Demands
Choose Natural Gas When:
- Pipeline gas tariffs are reliable and competitive.
- Floor space is limited, requiring a compact packaged system.
- The facility operates near urban areas with strict clean air and emissions rules.
- Fast steam response and automated operation are needed with minimal boiler room labor.
Choose Biomass When:
- Timber processing, rice milling, palm oil extraction, or agricultural operations generate low-cost combustible byproducts.
- The plant has adequate outdoor space for fuel yards, transfer conveyors, and ash silos.
- High annual operating hours (5,000+ hours/year) justify the higher initial capital expenditure.
- Regional environmental regulations permit solid fuel systems equipped with multi-cyclone or baghouse dust filters.
Choose Electricity When:
- Total steam capacity requirements remain below 1.0 to 2.0 TPH.
- Zero local combustion emissions are required (e.g., specialized pharmaceutical labs or clean food rooms).
- Low local industrial electricity rates or dedicated renewable power systems offset higher power draws.
- Exhaust stacks and fuel storage cannot be installed on-site.
For plants operating in Central Asia, read our market analysis on steam boiler price in Uzbekistan to see how local tariffs, pipeline routes, and solid fuel supply chains influence regional equipment selection.
13. How to Choose the Lowest-Cost Boiler Fuel
Follow this step-by-step engineering framework to select the right boiler fuel for your facility:
Frequently Asked Questions For Steam Boiler Fuel Cost
How much does it cost to produce one ton of steam?
Direct fuel costs typically range from $18 to $35 per ton for solid biomass systems, $28 to $45 per ton for natural gas boilers, and $60 to $90+ per ton for electric units. Exact production costs depend on your local fuel tariffs, boiler thermal efficiency, feedwater temperature, and condensate recovery rates.
Is gas cheaper than biomass for generating industrial steam?
In most regions, biomass delivers lower fuel costs per ton than natural gas, especially near agricultural or timber processing centers. However, biomass boilers require a higher upfront investment for fuel conveyors, storage yards, and dust collectors, and demand more auxiliary electricity and operating labor.
Why are electric steam boilers expensive to run for large plants?
Producing one ton of steam requires roughly 680 to 730 kWh of electricity. With standard industrial electricity tariffs at $0.08 to $0.14 per kWh, fuel costs run from $55 to $100 per ton of steam. These utility expenses make electric boilers uneconomical for large, continuous industrial processes.
How can factories lower their boiler fuel consumption?
1.Add an economizer to lower flue gas exit temperatures below 80°C.
2.Return hot condensate to the deaerator to reduce cold makeup water demand.
3.Tune burner air-fuel ratios with an oxygen trim system (aim for 3% to 4% excess O₂).
4.Maintain proper water treatment to prevent heat-insulating scale on internal tubes.
5.Insulate all distribution steam valves, pipes, and flanges.
How do I calculate steam cost per ton?
Determine the energy needed to turn feedwater into steam at your working pressure, divide that by your boiler’s thermal efficiency, and multiply by your local fuel price. Add the cost of auxiliary electricity, makeup water, softening chemicals, maintenance, and operating labor to calculate your total cost per ton.
What is the typical thermal efficiency of an industrial steam boiler?
Standard natural gas boilers without heat recovery achieve 88% to 91% efficiency. Adding a condensing economizer boosts efficiency to 94%–98%. Solid biomass boilers run at 80% to 86% efficiency, while electric steam boilers reach 98% to 99% conversion efficiency at the heating elements.
Get a Custom Steam Cost & Fuel Selection Analysis
Need help choosing the most economical boiler fuel for your factory? Our engineering team will review your project parameters to calculate your actual cost per ton of steam:
- Target Steam Demand (TPH or kg/h)
- Required Working Pressure (MPa or bar)
- Local Delivered Fuel Tariffs (Natural gas, diesel, wood chips, pellets, or electricity)
- Daily Operating Hours & Condensate Recovery Estimates
- Project Destination & Emissions Requirements
We provide detailed fuel consumption models, balance-of-plant auxiliary equipment scopes, and 5-to-10-year lifecycle TCO calculations to identify the lowest-cost steam system for your plant.